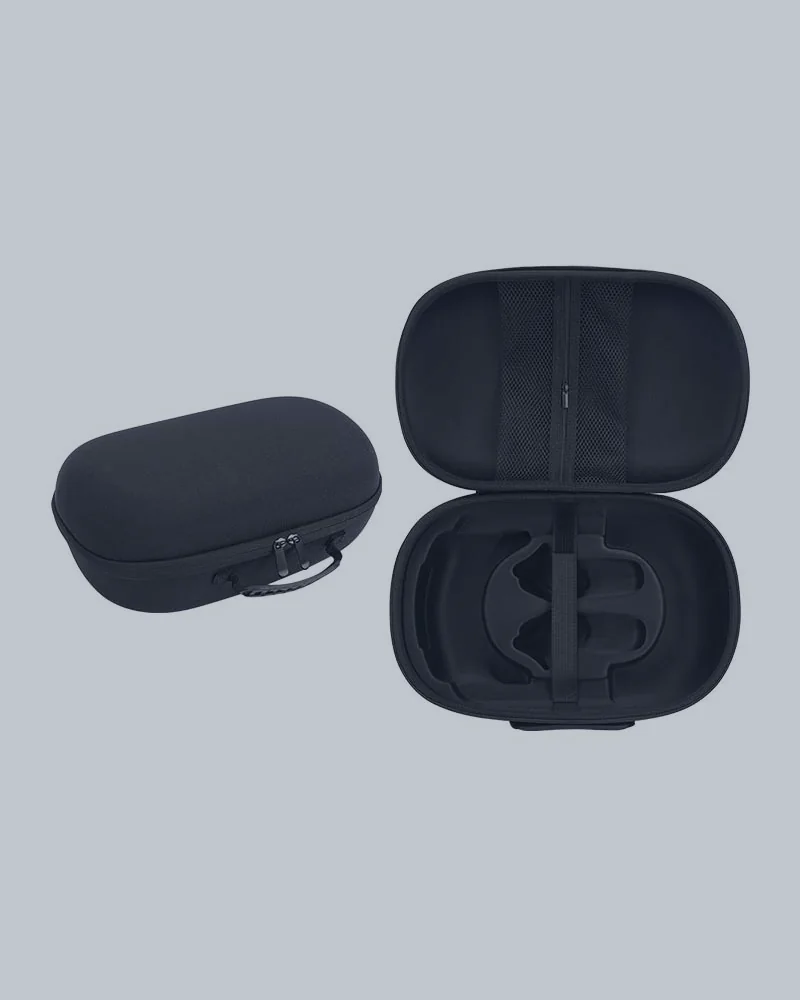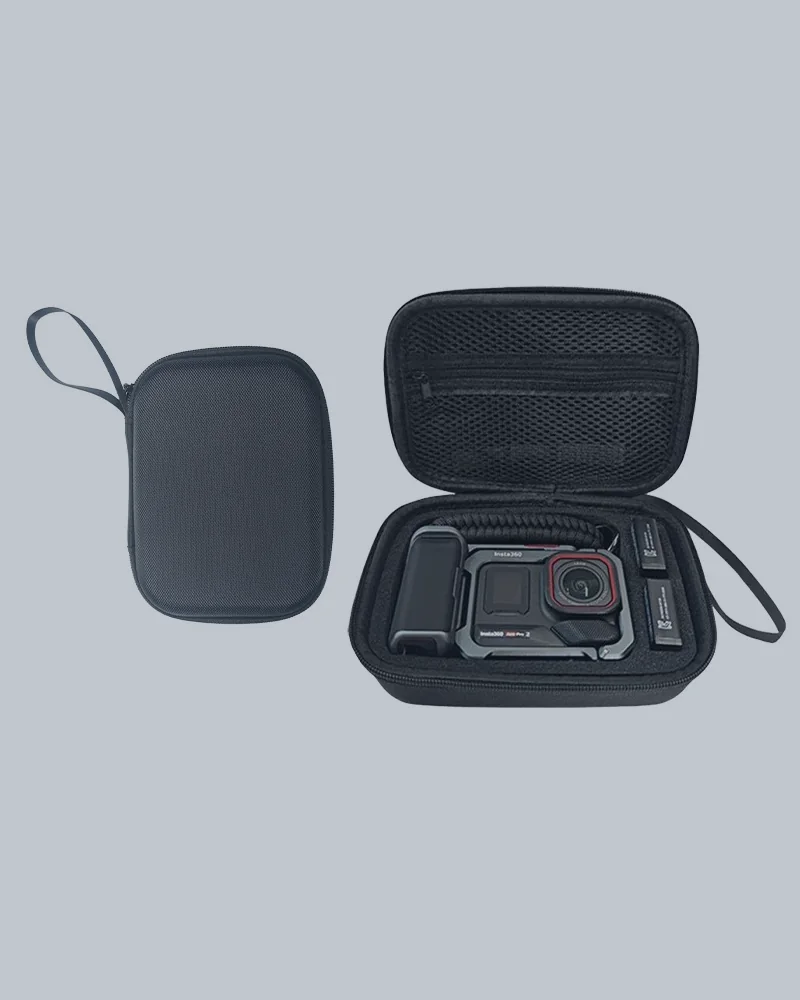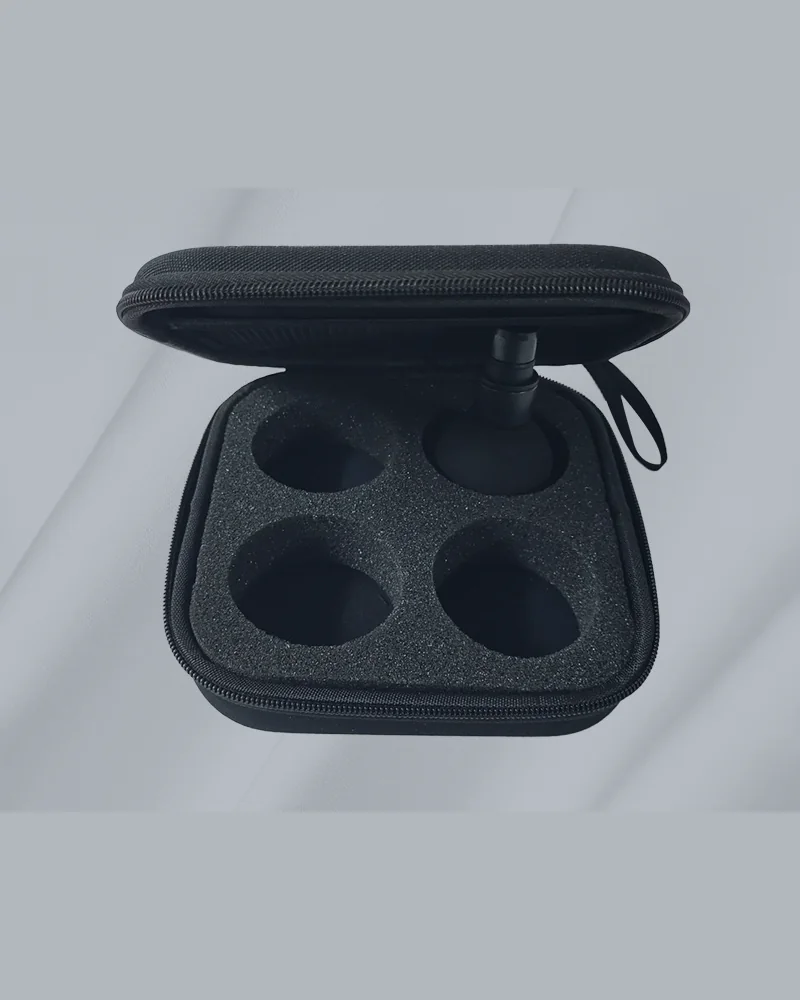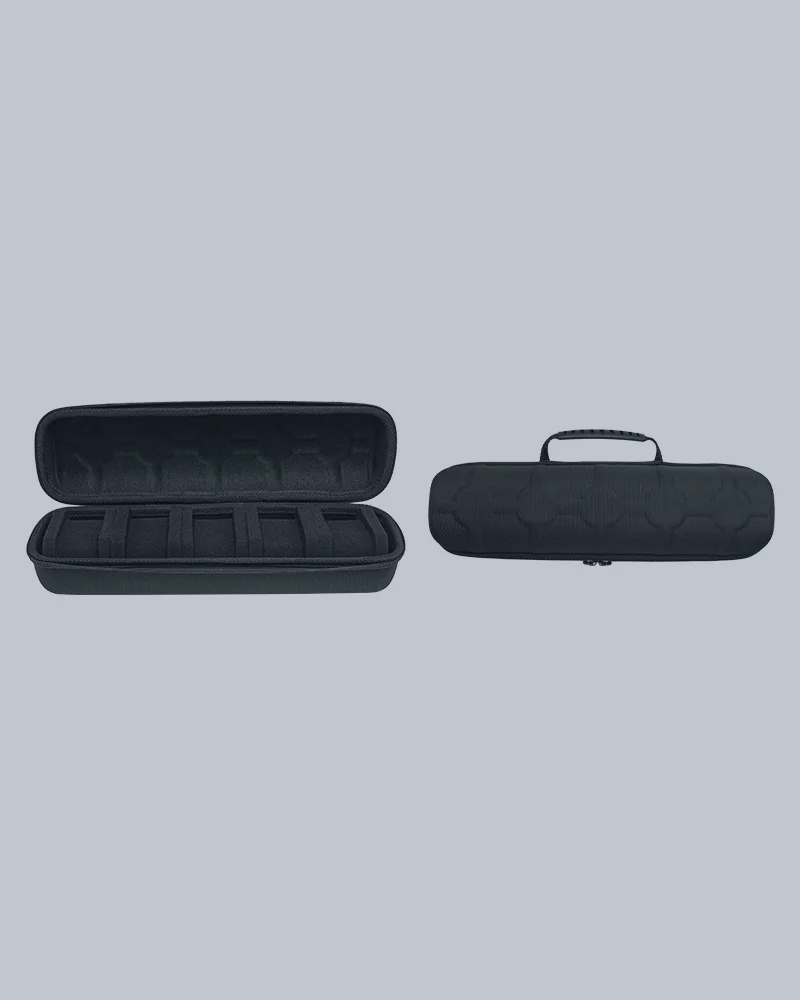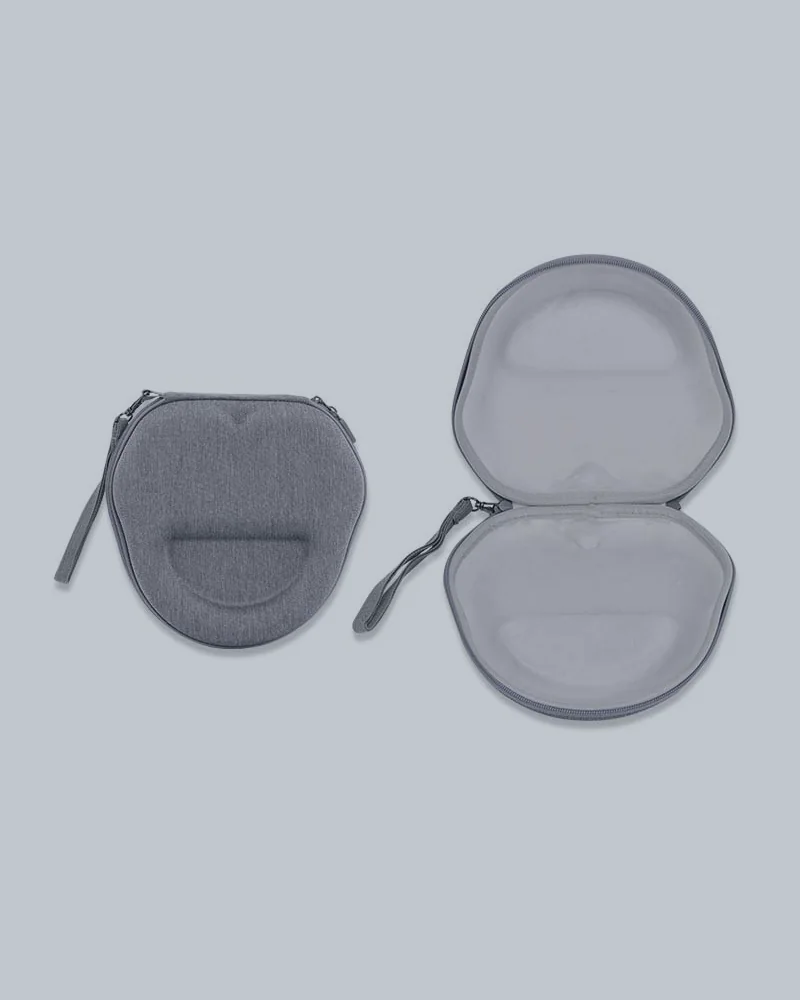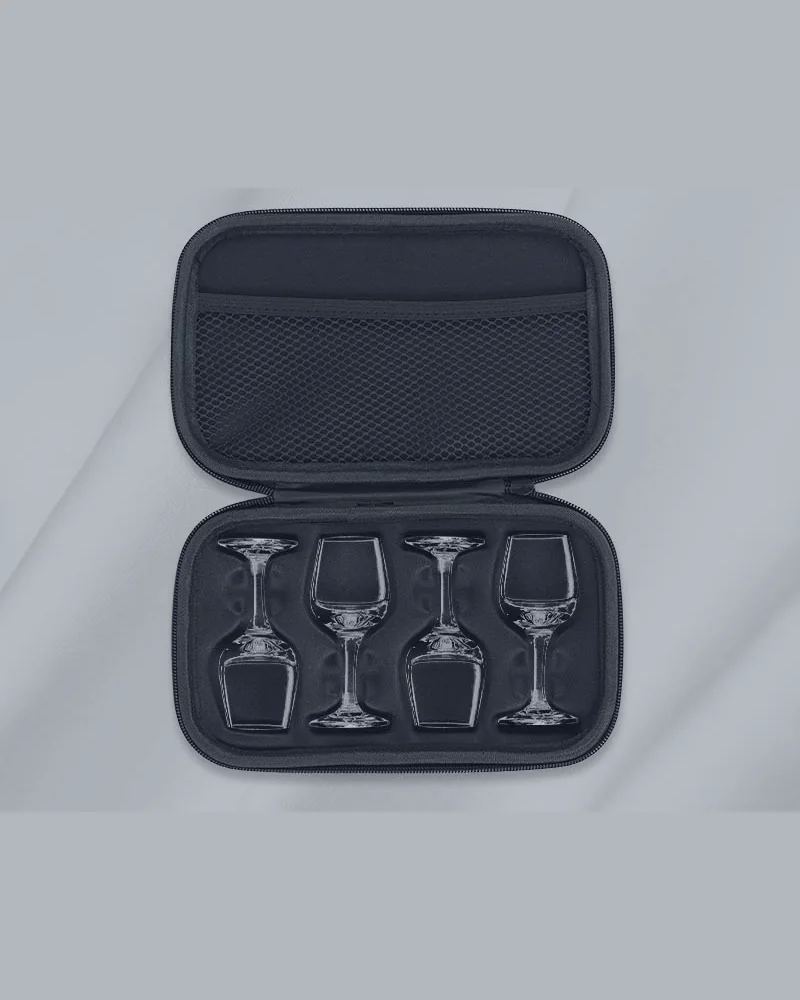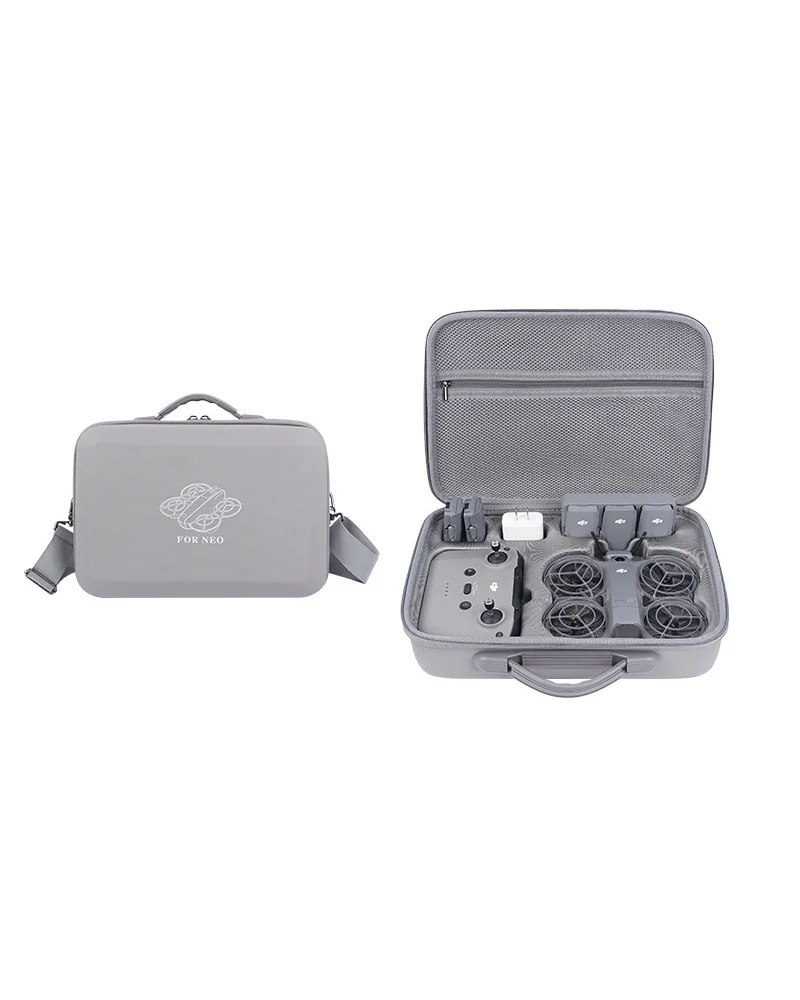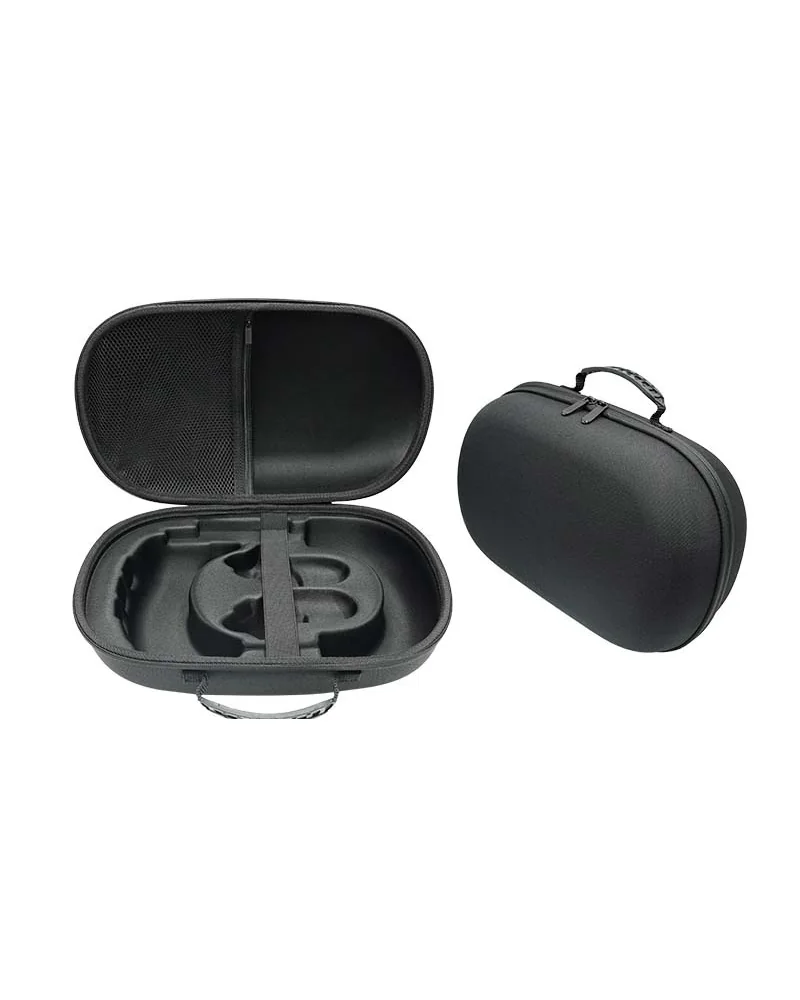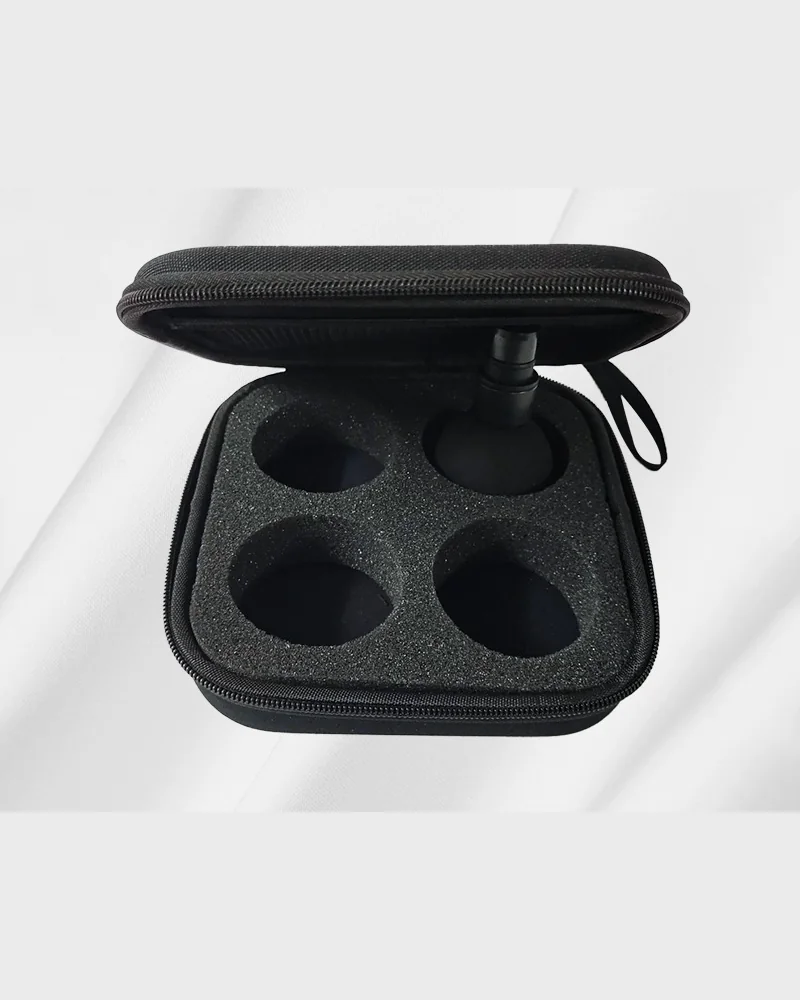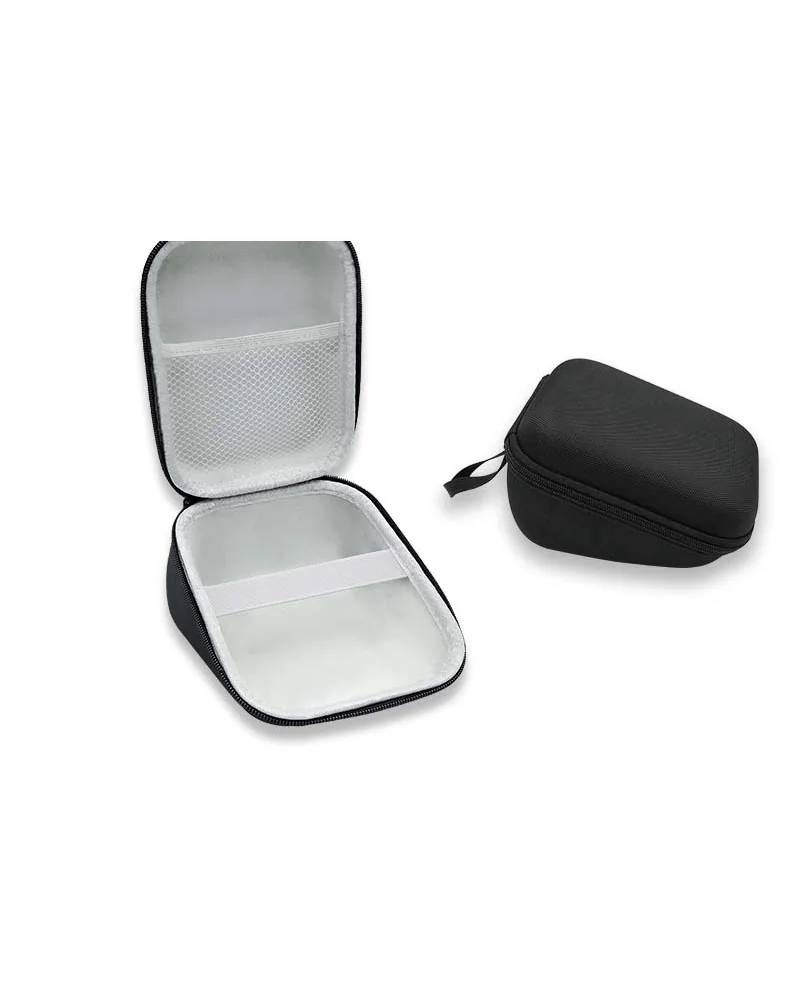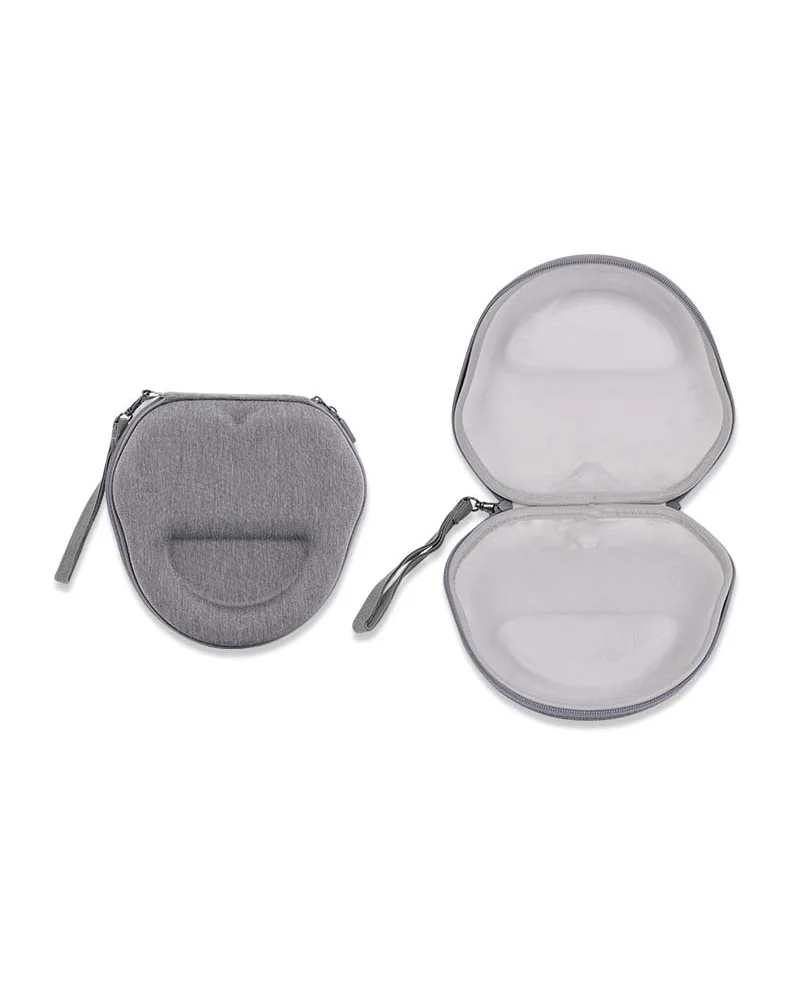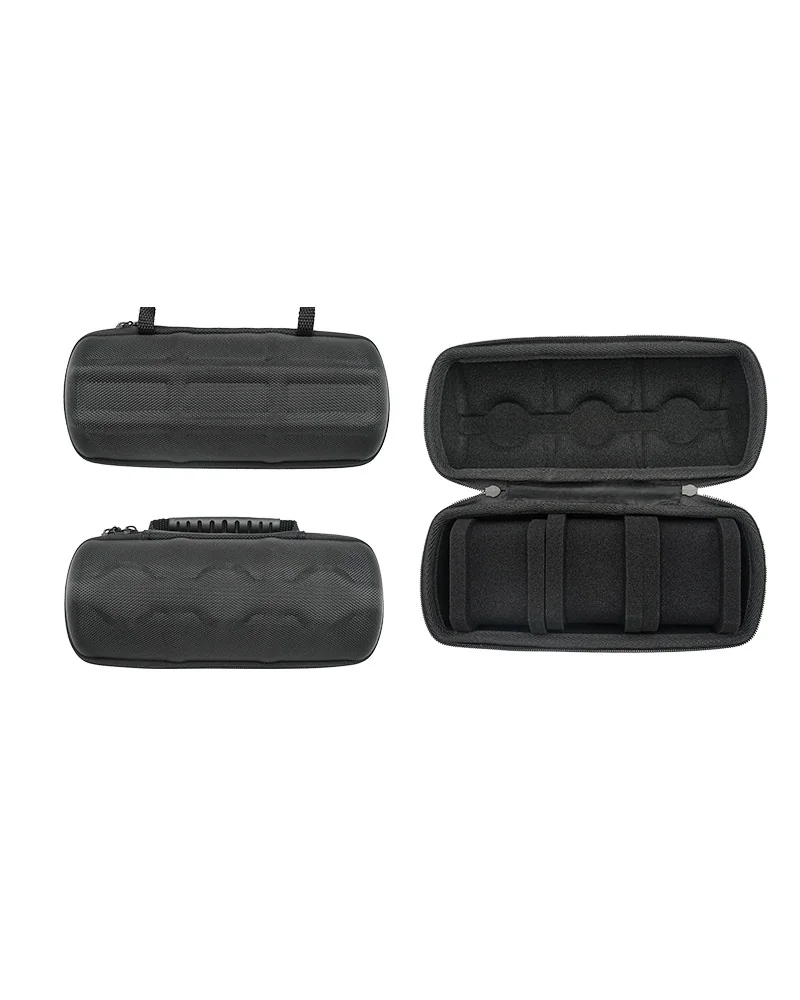
Moulded EVA hard case with a custom foam insert

Custom EVA Case & Hard Shell Manufacturer in Dongguan

Custom Hard Case moulds EVA storage cases for drones, VR headsets, cameras, tools, medical devices and consumer electronics — 300+ moulds on file, die-cut foam inserts, your logo and retail packaging. MOQ 300 pcs per style.

MOQ 300 pcs/style · Sampling 7–10 days · Production 20–30 days

How it is built

How an EVA case is built

Three decisions fix the product before a single shell is pressed: the shell, the insert and the finish. Each one has its own tool, its own tolerance and its own line on the quotation.

Moulded EVA shells

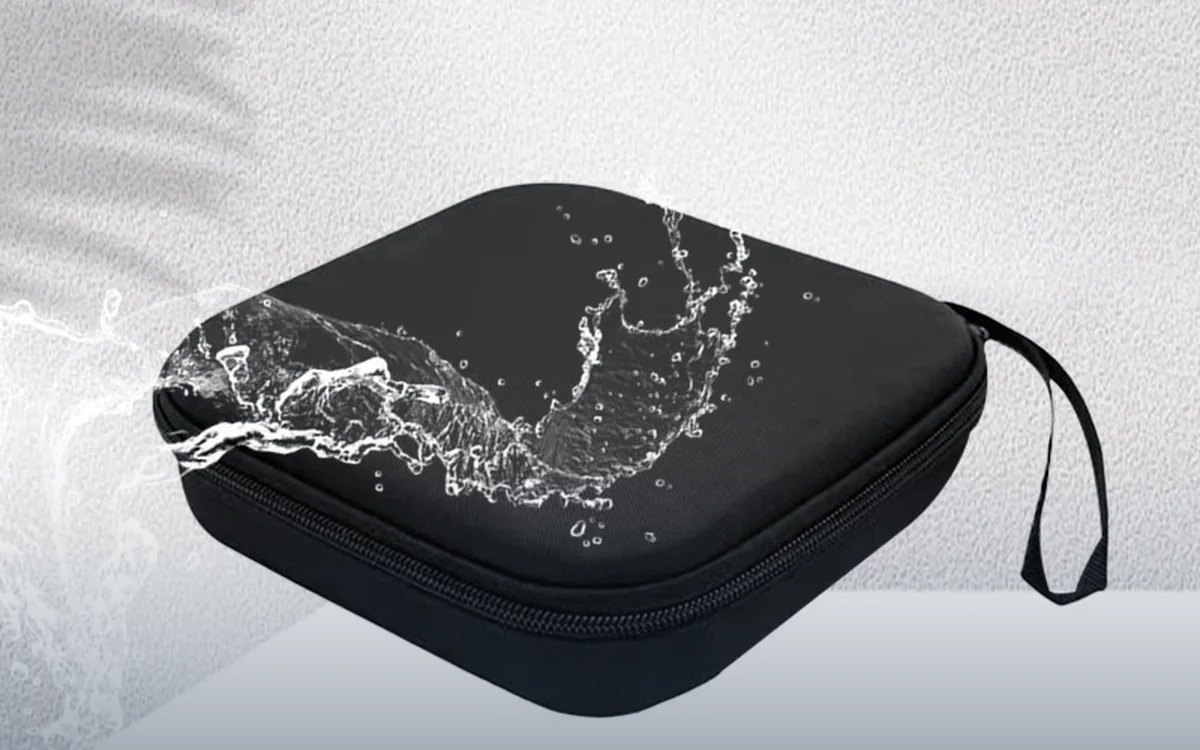
A 5 mm EVA shell laminated to 1680D nylon, 600D polyester or PU leather, pressed over an aluminium tool at 160–180 °C — rigid walls, controlled corner radius, ±1.5 mm.

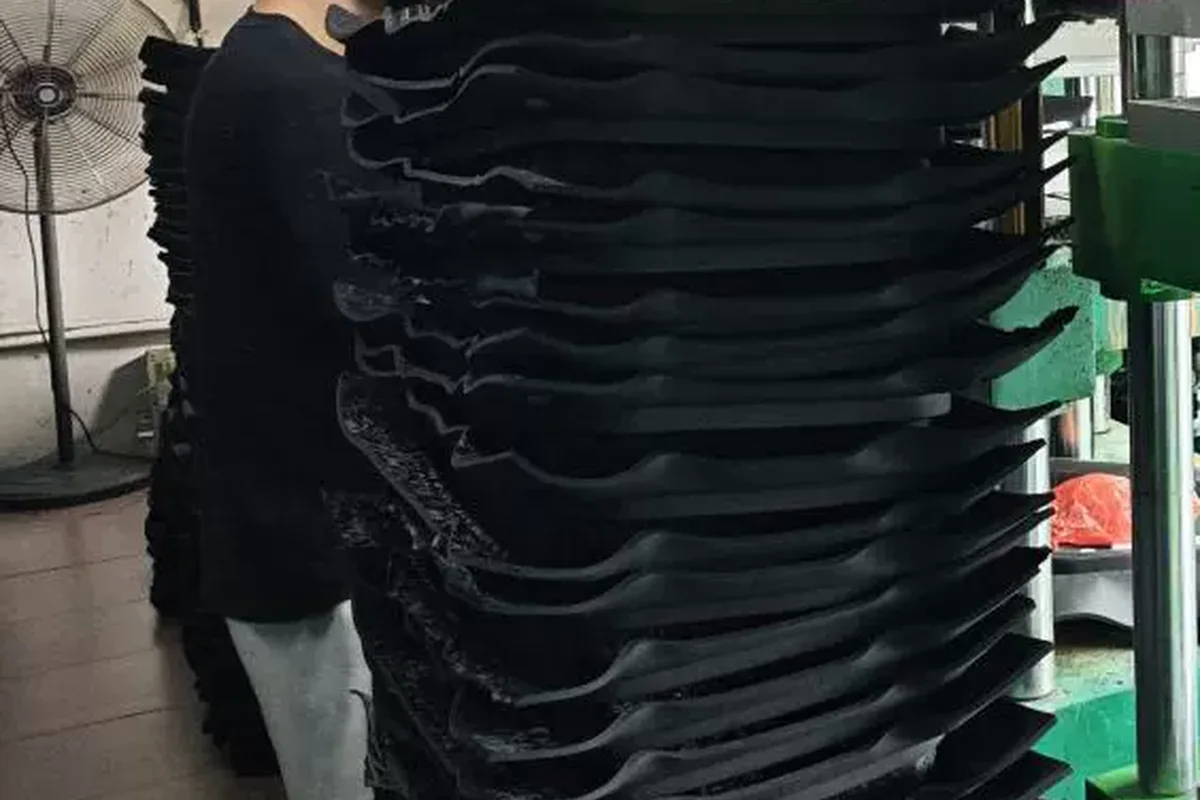
From sheet to shell

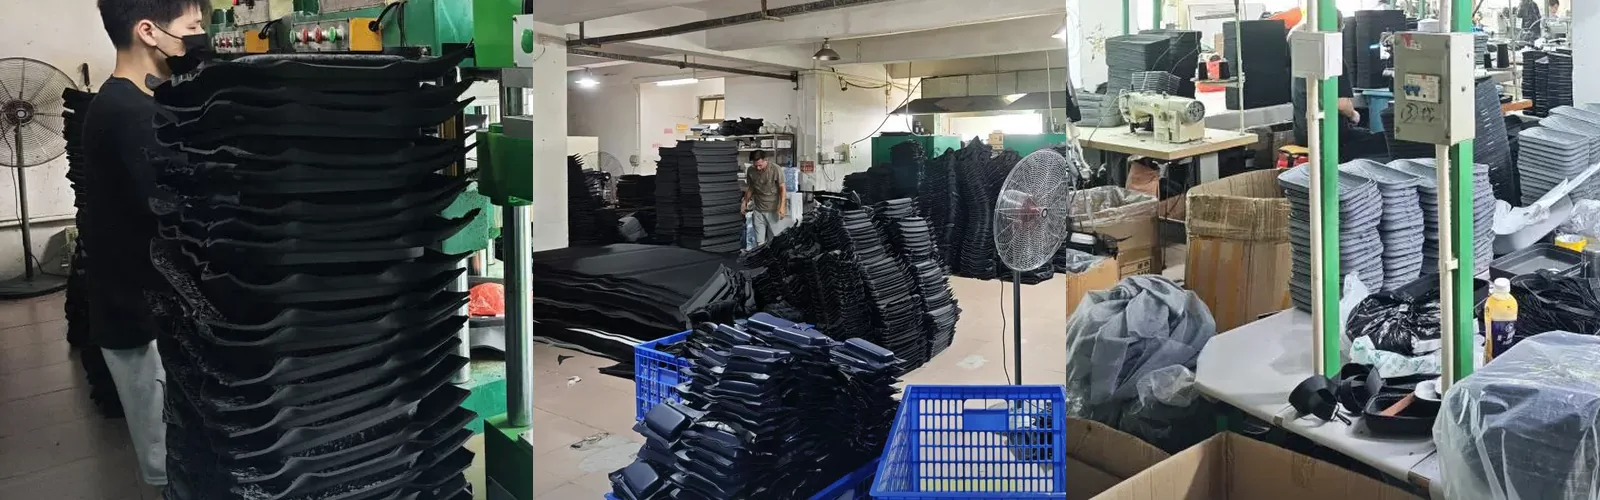
Every shell starts as a flat sheet cut to pattern, then pressed and cooled in the tool. The mould stays on file with its cavity dimensions, so a reorder runs from the same tool in 7–10 days.

How we mould a case
Die-cut foam inserts

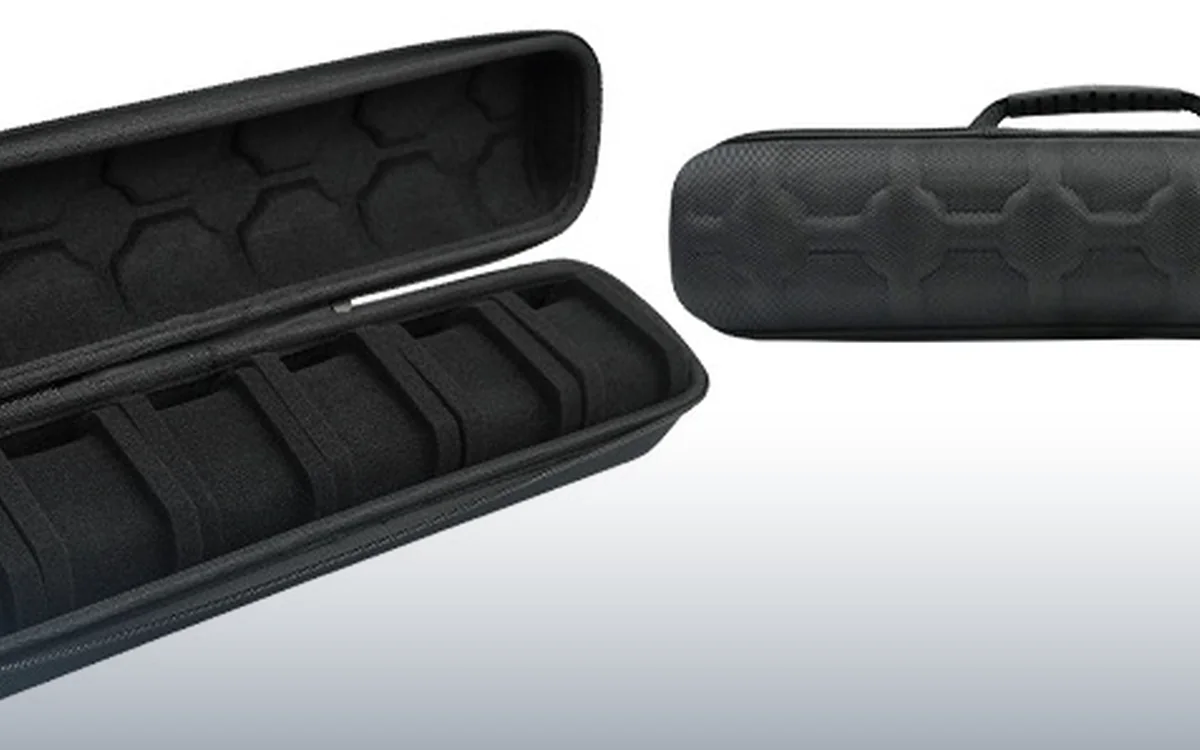
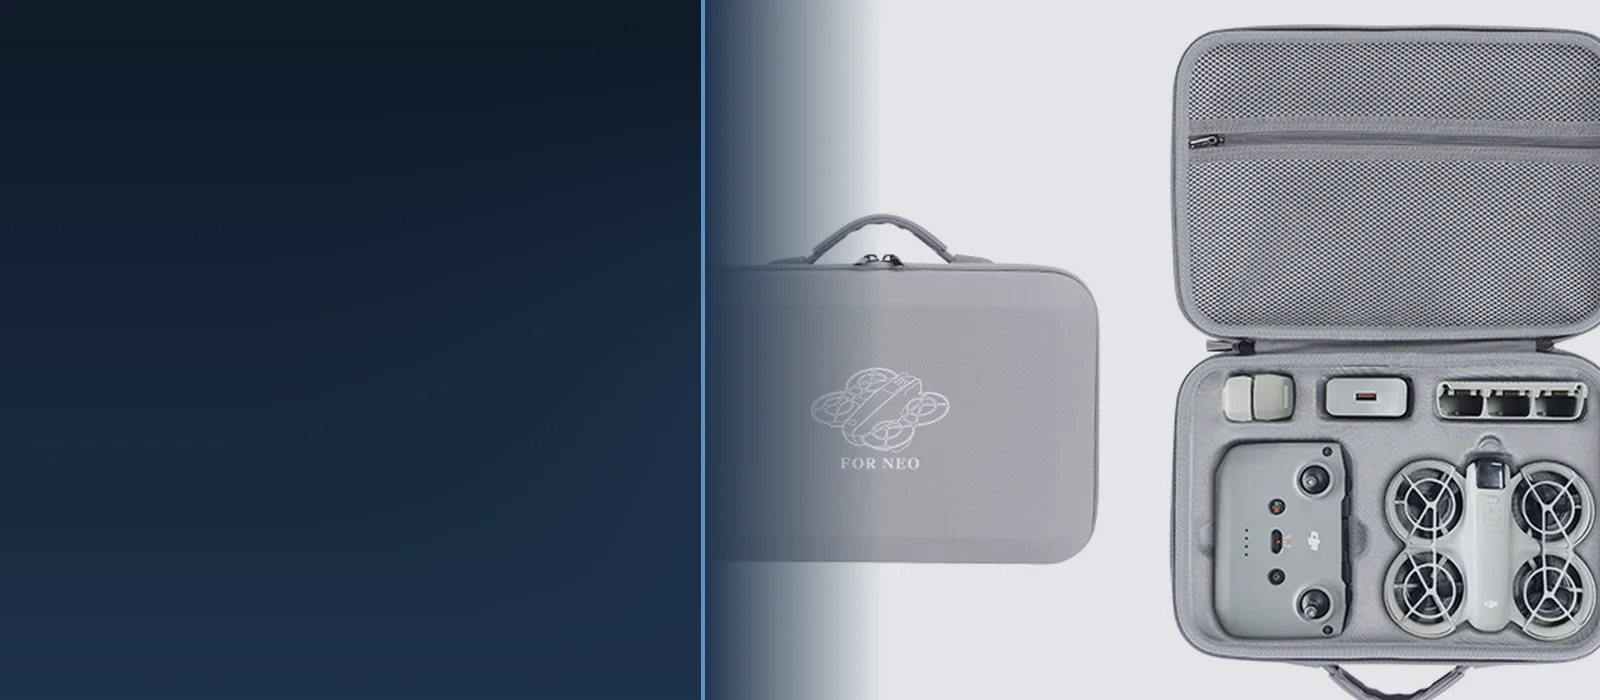
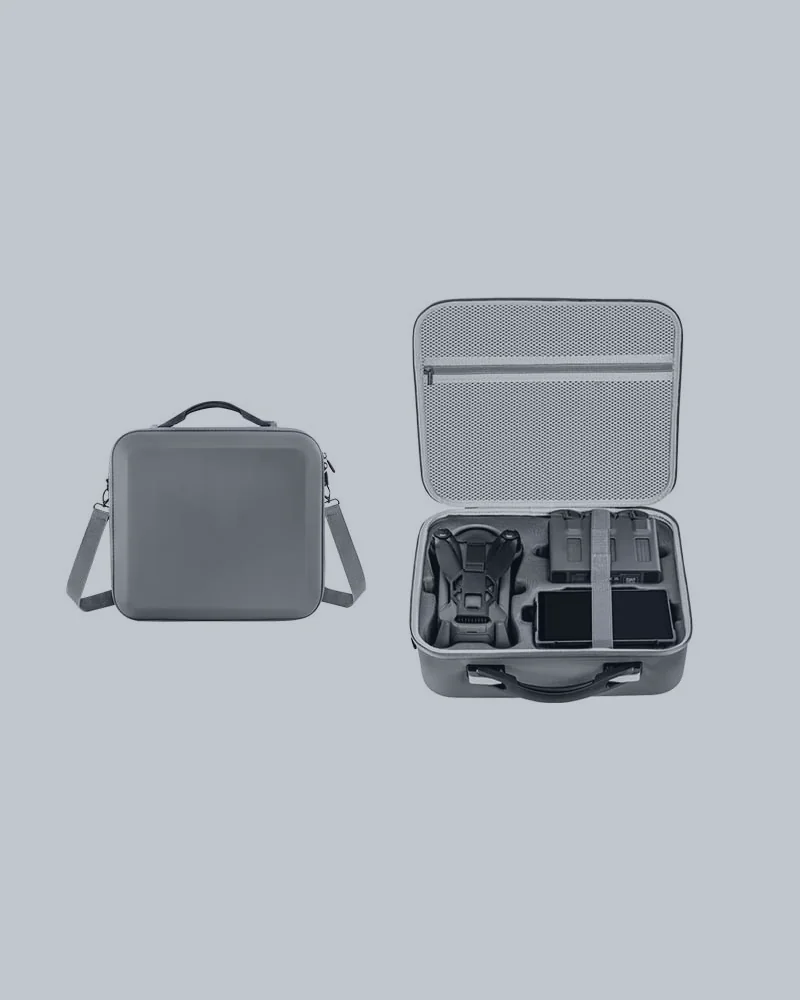
Every cavity is cut to the device outline at ±2 mm, with a 10 mm base pad under heavy items, so the device cannot move when the case is carried or dropped.

Three insert systems

Die-cut EVA, pick-and-pluck foam or a thermoformed tray — the choice moves the tooling cost, the minimum order and how firmly the device is held in the cavity.

Compare insert types

Private label finishing

Embossed logo, heat transfer, silk screen, a metal plate or a rubber patch — applied in the same plant as the shell, with your zipper puller, hangtag and carton marks.

One plant, one shipment

Logo, zipper puller, hangtag and carton marks are finished on the same floor as the shell, so the branding and the packaging leave in the same container instead of meeting at a forwarder.

Private label options
Cost drivers

Why the insert decides the cost

Two cases can cost the same per unit and protect nothing alike. The insert, the tooling behind it and the packaging around it are where the money actually goes.

The cavity, not the fabric

A 2 mm cavity error is the difference between a device that sits still and one that rattles in a courier van. Insert cuts hold ±2 mm with a 10 mm base pad; re-cutting a die is US$150–300.

Tooling is a line, not a surprise

A new shell mould is US$600–1,400 and an insert die US$150–300, both credited back against 2,000 pcs. Where a shell already on file fits the device, that line is zero.

Packaging adds US$0.20–2.50

Polybag and insert card sit at the low end, a printed sleeve or rigid gift box at the top, with the barcode or FNSKU label applied before the carton is sealed.

About us

An EVA case factory in Shijie, Dongguan

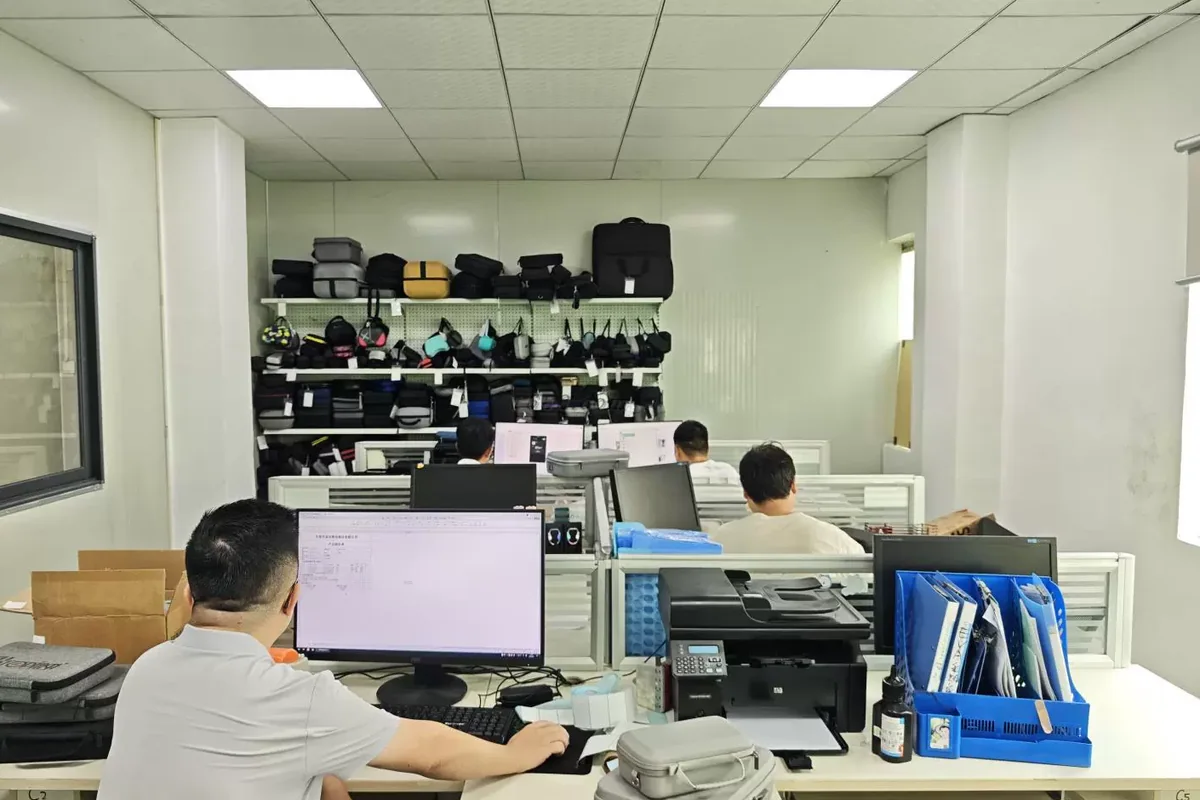
Custom Hard Case has been pressing EVA shells in Shijie Town since 2015 — first for case traders, then for drone, VR, camera, tool, medical and electronics brands in 35+ countries. The tool room, the moulding presses, the foam cutting room, six stitching lines and the logo stations all sit on one 4,200 m² floor.

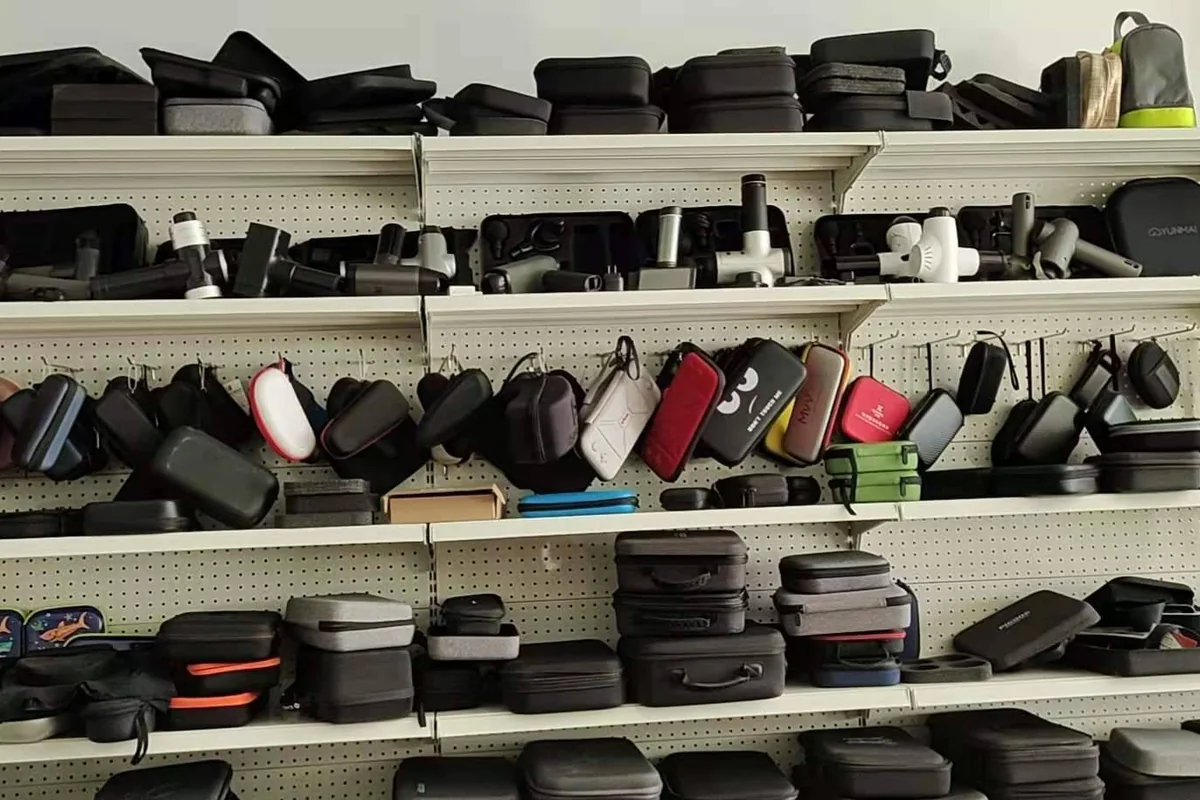
That layout is why a change to a cavity or a zipper does not become a two-week email chain. We hold 300+ moulds on file, and more than half of the orders we ship are reorders against a mould that is already on file.

About us   Contact us
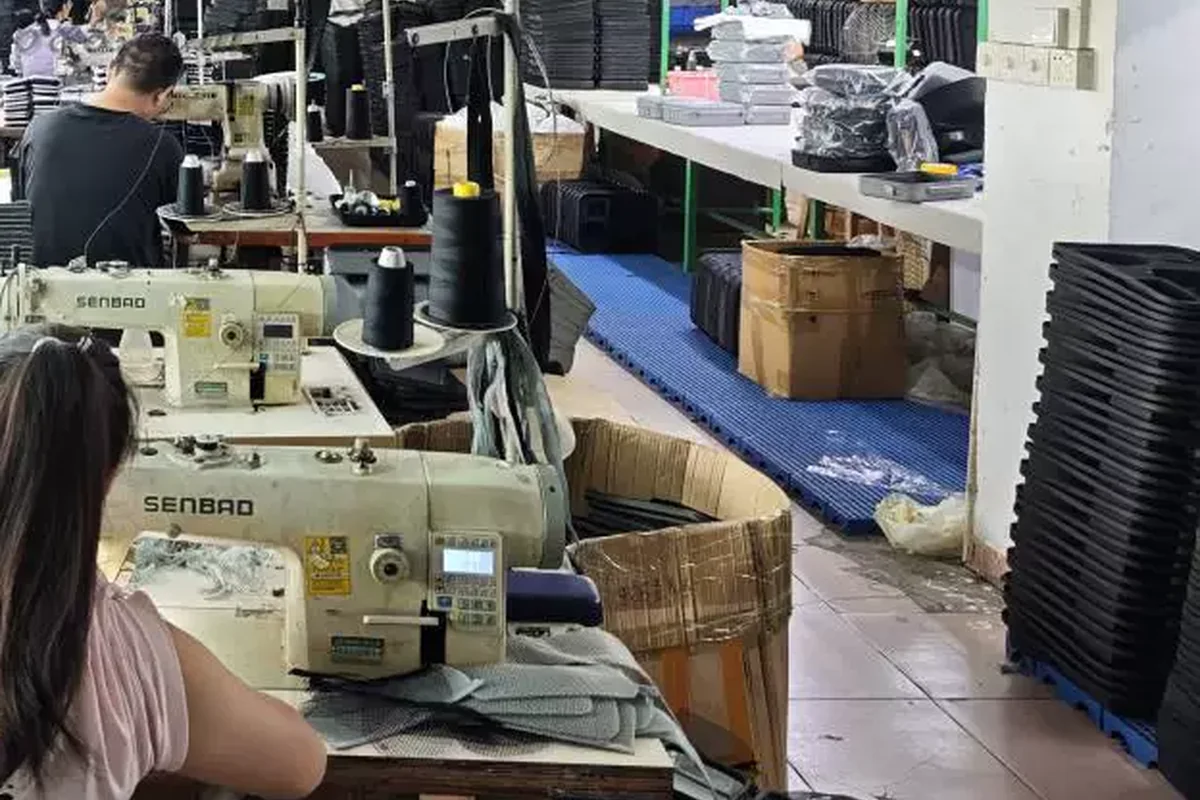
Stitching line at the Dongguan EVA hard case factory
Custom hard case supplier

A case is a specification, not a fabric choice

Two cases can look identical on a product page and behave nothing alike in a courier's van. The difference is the wall thickness, the insert tolerance and the zip. We quote those three line by line, so you can see what you are paying for before the mould is cut.

  • MOQ: 300 pcs/style
  • Sampling: 7–10 days
  • Production: 20–30 days
  • Capacity: 150,000 pcs/mo

Talk to our team

Current programmes

Cases running through the plant

A sample of active programmes. Any of them can be re-pressed in your face fabric, lining, insert layout and branding.

View all products

Looking for a case manufacturer you can reorder from?

Send the device or kit you need to pack, the quantity and any logo files. You will get a mould match, a costed quotation and a sampling date within one working day.

Ways to start

Three ways brands work with us

Whether you have a CAD file, a physical device or only a reference photo, there is a route that fits your stage.

Start from a stock mould

Start from a stock mould

Choose one of 300+ shells already on file, add your face colour, logo and insert legend, and sample in 7–10 days without paying for tooling.

Send your design
Build a private label case

Build a private label case

Our shells, cut and finished under your brand, with your logo, zipper puller, hangtag and retail packaging in the same run.

Make private label
Develop a new mould

Develop a new mould

Send a CAD file or a physical unit. We cut a new insert and shell mould in 15–20 days, and credit the tooling against 2,000 pieces.

Start a mould project
EVA moulding, foam cutting and stitching floor

From flat EVA sheet to sealed carton

Four stages, one quality gate at each — and a photo report before your goods leave Dongguan.

Mould and shell

EVA sheet is laminated to your face fabric, then compression moulded around the shell tool at 160–180 °C. ±1.5 mm on the finished cavity.

Insert cutting

Foam inserts are die-cut from a CAD file or a device mock-up, with ±2 mm on the cavity and a 10 mm base pad under heavy items.

Stitching and finish

120+ operators stitch zips, handles and straps on 6 lines, then trim, clean and inspect every unit before it reaches packing.

Trimming and finishing

Every unit is trimmed, cleaned and inspected against the drawing, then bagged with your insert card, hangtag or printed sleeve.

Journal

Sourcing, materials and costing guides

What we have learned producing moulded cases for 35+ markets — written for buyers, not for search engines.

All articles

Factory-direct price

Moulding, foam cutting, stitching and packing under one roof, so there is no trading-company margin between the press and your carton.

Checked before it ships

AQL 2.5 inspection, a dimensional audit and a photo report of the packed cartons before the container is sealed.

Materials you can verify

1680D, 600D, PU and EVA from named suppliers, with REACH and RoHS test reports available on request for each lot.

Dates that hold

Sampling in 7–10 days on a stock mould, production in 20–30 days, and a written ship date in the order confirmation.